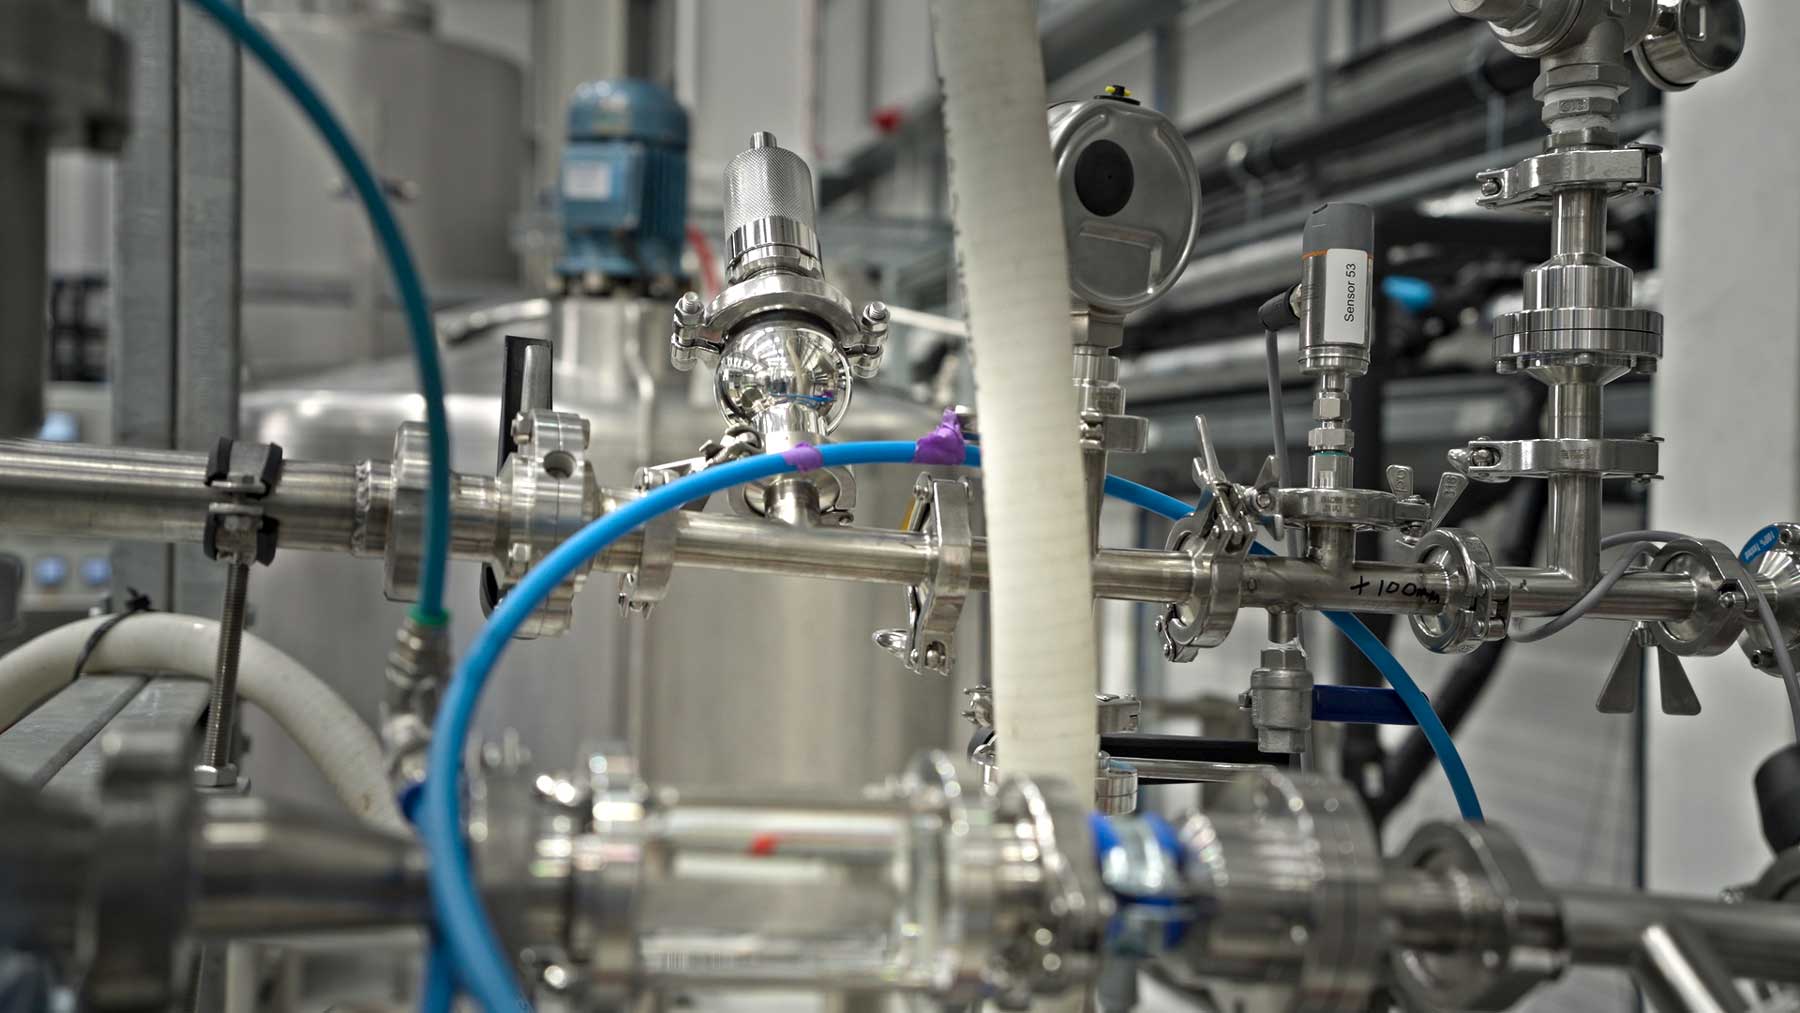

Supablu is powered by our proprietary modular photobioreactor system: a closed, precision-controlled environment that allows us to produce natural, functional ingredients at industrial scale, anywhere in the world.
This system redefines ingredient manufacturing, delivering consistency, scalability, and sustainability without compromise on quality or cost.
Our photobioreactors are modular by design. They can be replicated and deployed close to or on-site with production partners, reducing your food miles and ensuring a secure, resilient ingredient supply. Tapping into your own waste streams offers a carbon mitigation tool, unmatched in the colourant sector.
By producing at the point of need, Supablu offers food manufacturers a truly local source of natural colour: globally available, locally produced.

Each unit integrates with existing industrial infrastructure, using waste heat and captured CO₂ from collaborators to fuel microalgae growth. This approach reduces both operating costs and carbon footprint, setting a new standard for sustainable ingredient manufacturing.
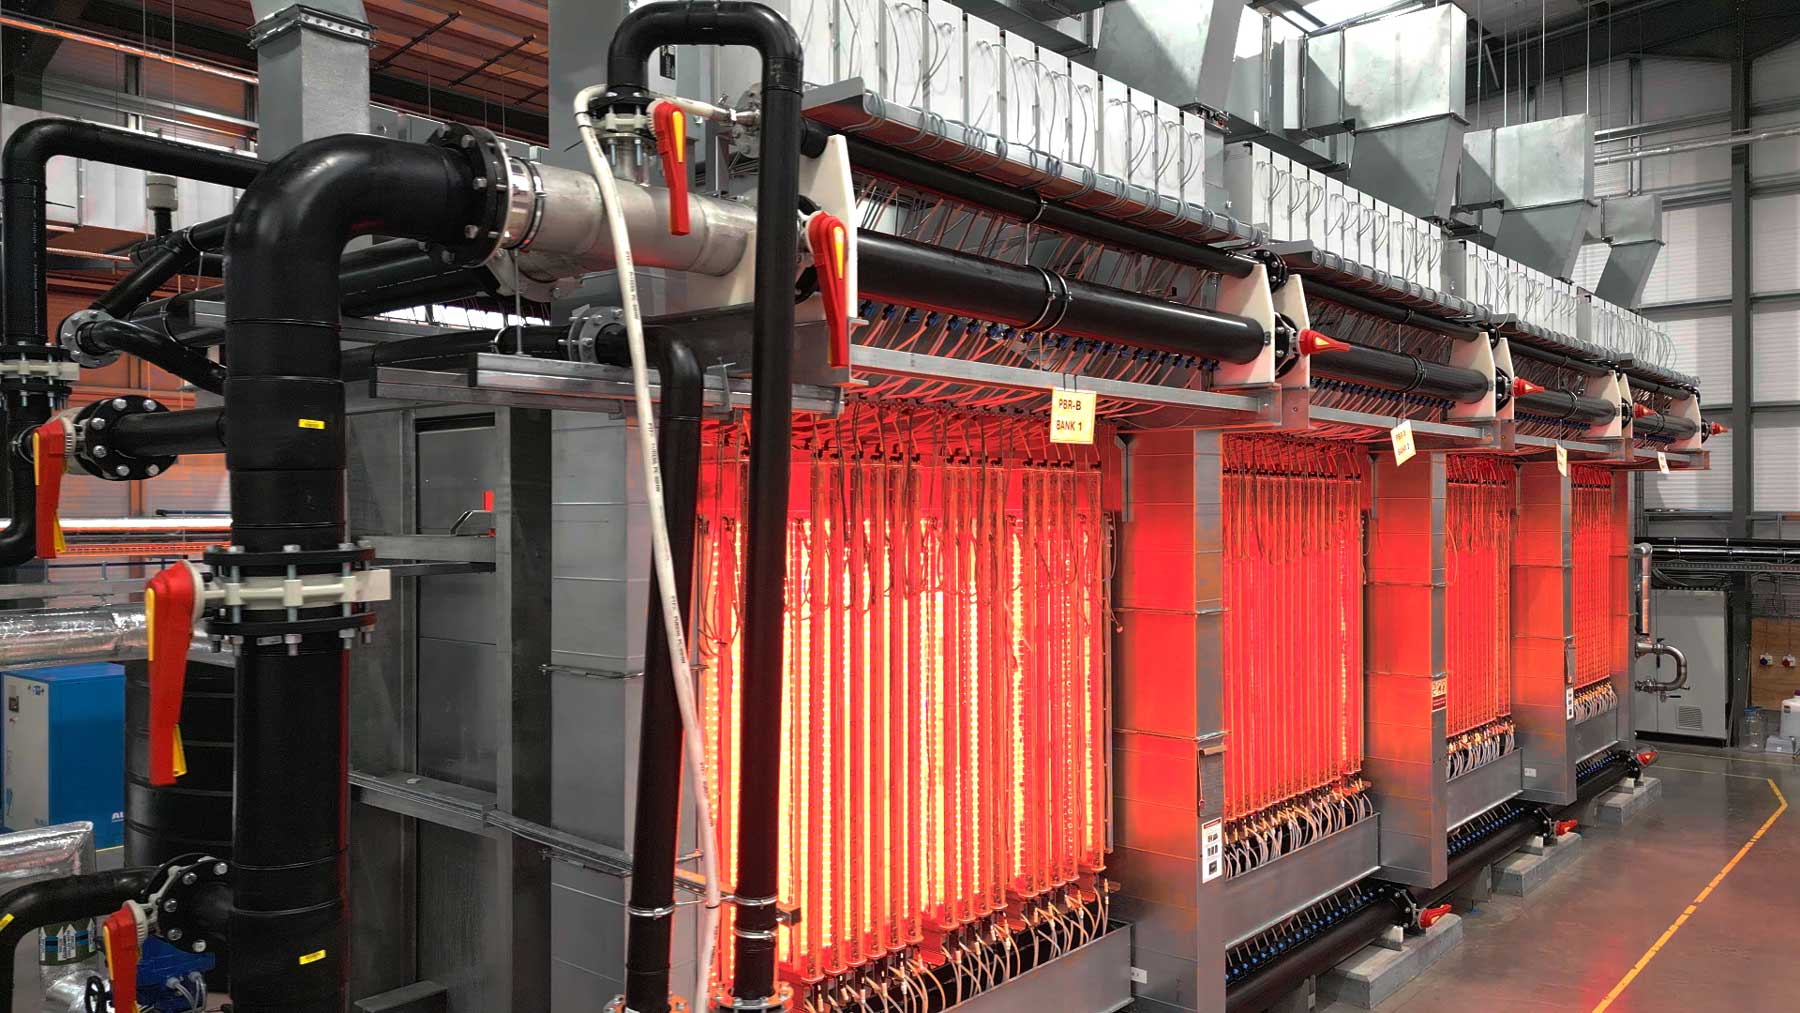
Unlike open “race-way” pond systems, our closed photobioreactors maintain complete control over light, temperature, and nutrient balance - guaranteeing a pure, stable, and reproducible pigment every time. Customers can be confident in consistent, high-quality production, free from pesticides, animal intrusion, and the variability of sunlight.
Supply chain concerns linked to overseas sourcing, including Chinese or geographically constrained supply and quality issues, are completely removed. That precision ensures Supablu delivers the same vibrant, high-performance blue across every batch, every application, and every market.